 EN
How to Reduce Film Waste with a Premade Pouch Packaging Machine?
2026/09/20
Premade Pouch Machines: Reduce Film Waste, Cut TCO & Achieve Faster ROI

2026/10/08
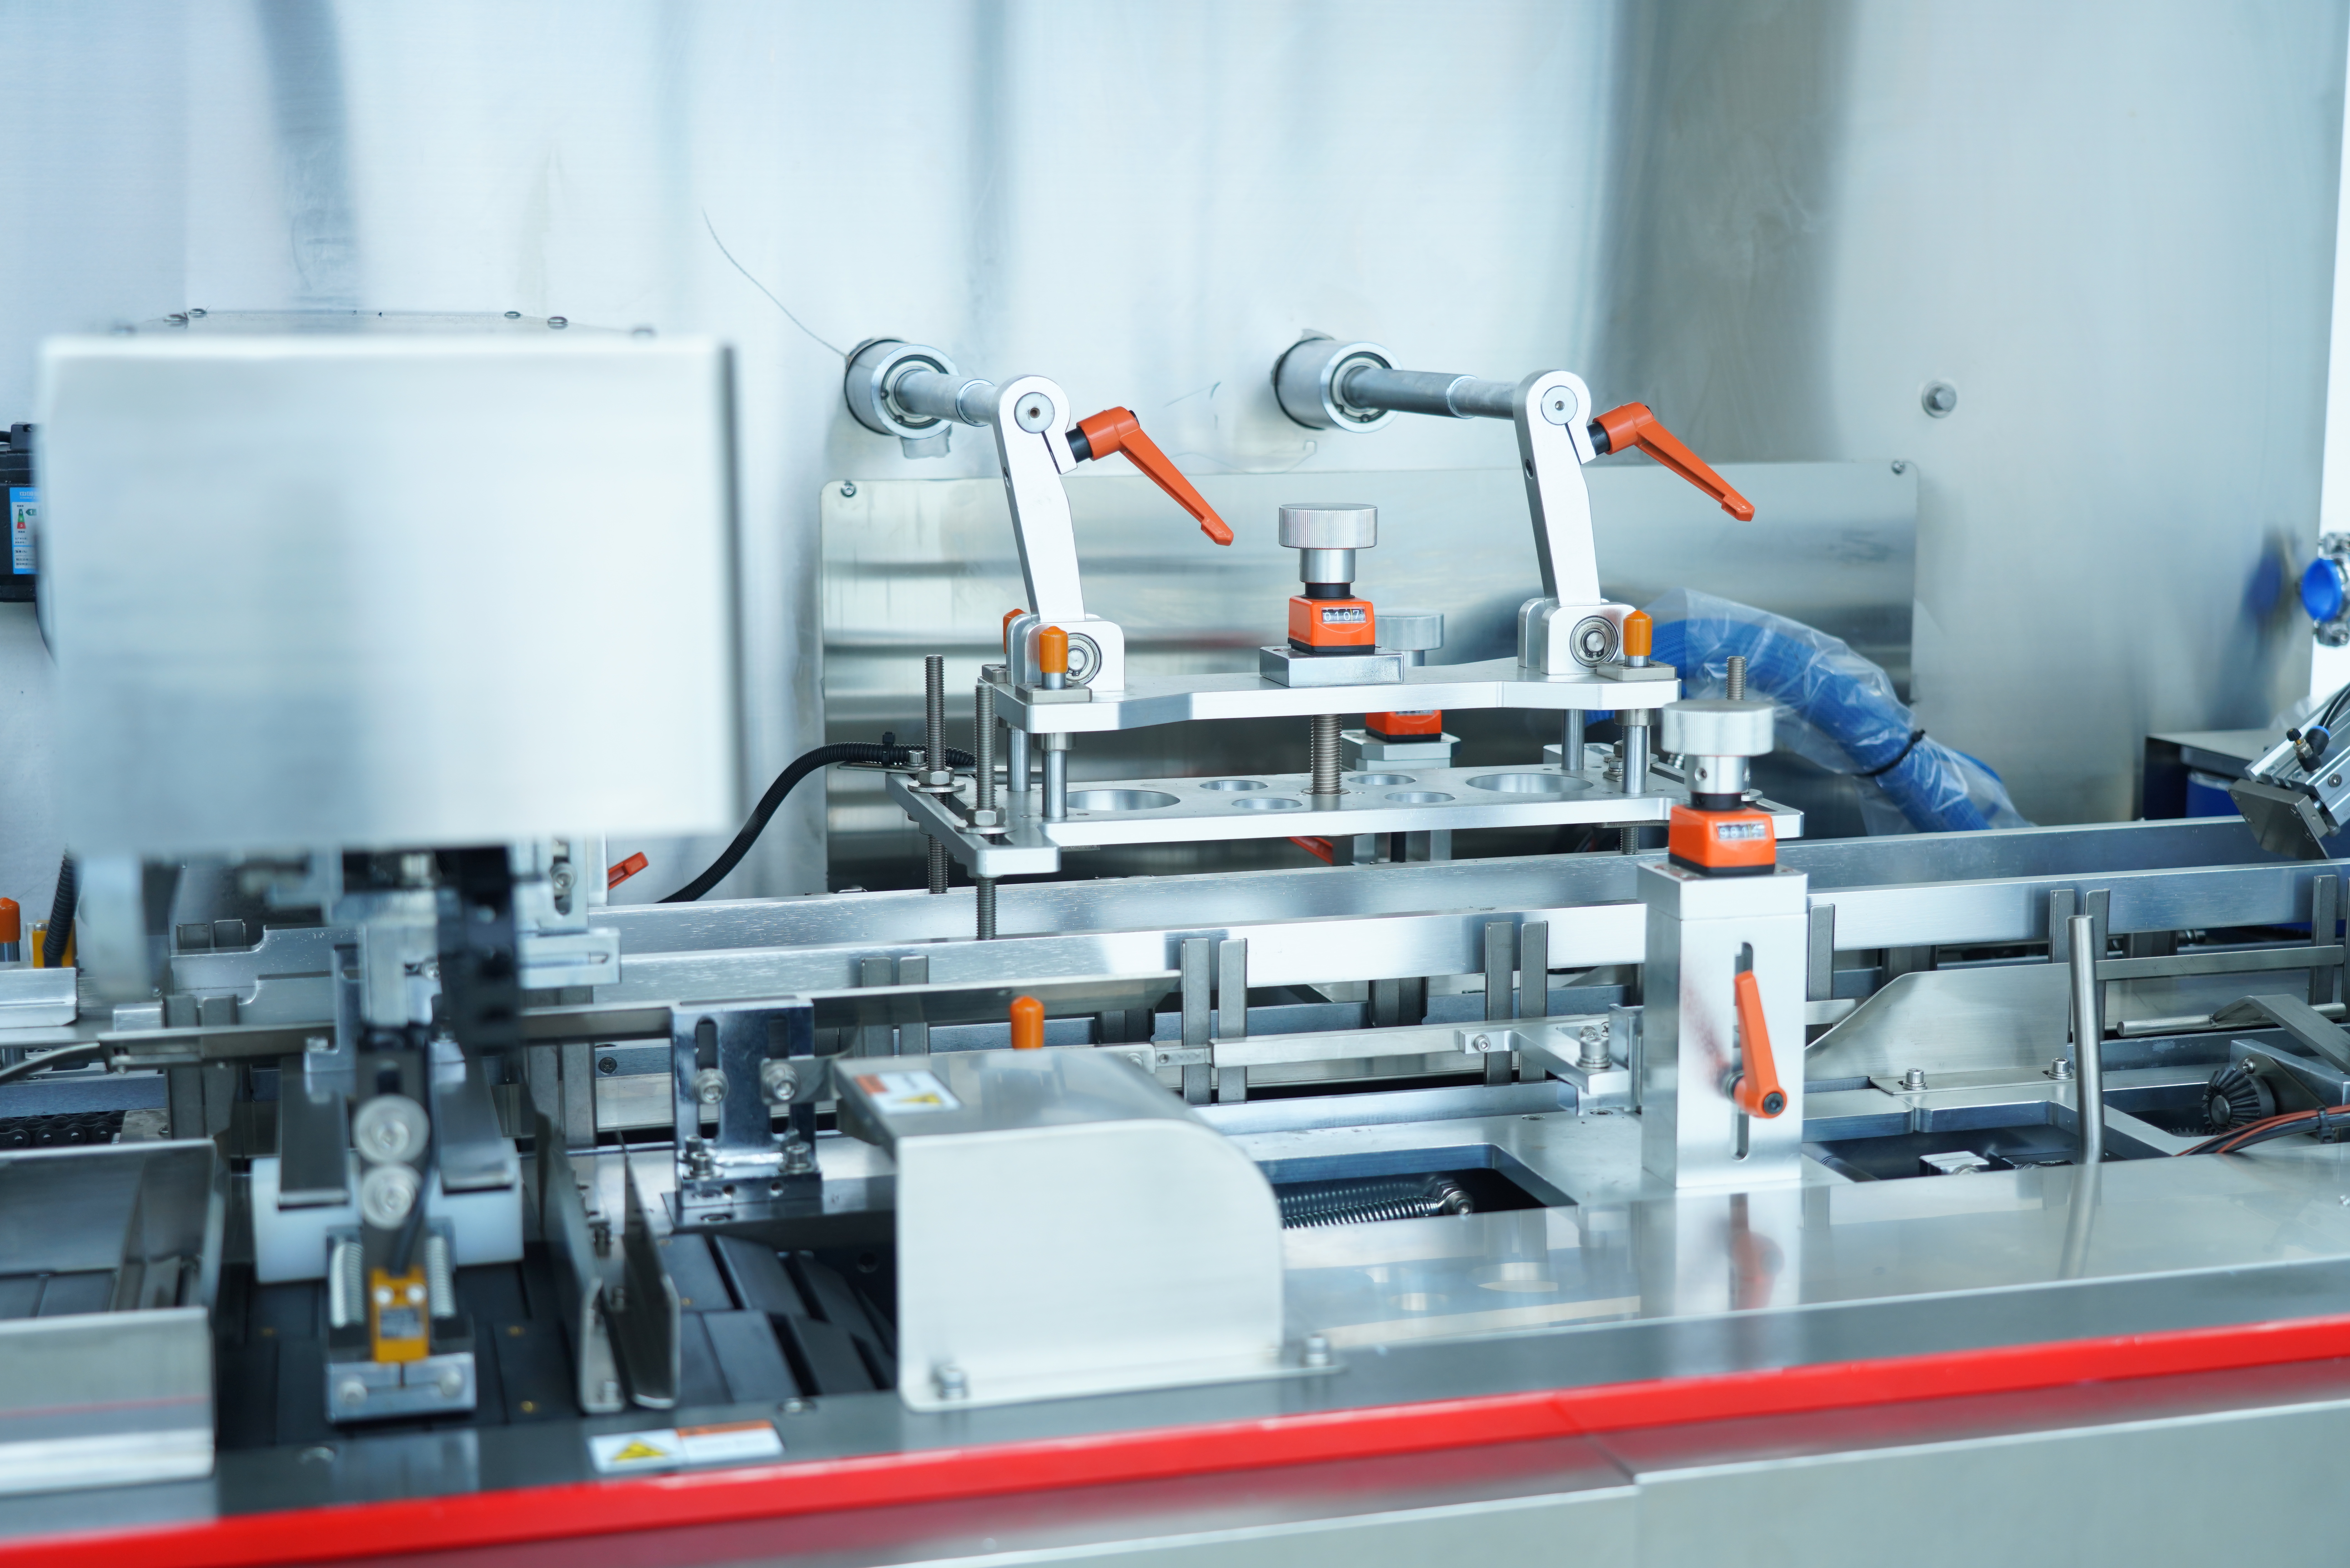
The modern packaging industry relies heavily on efficient solutions to meet growing demand and maintain competitive advantage. A carton box packing machine has become essential for manufacturers and distributors seeking to automate their production workflows. Understanding the different types available helps businesses make informed decisions about which carton box packing machine best suits their operational requirements and budget constraints.
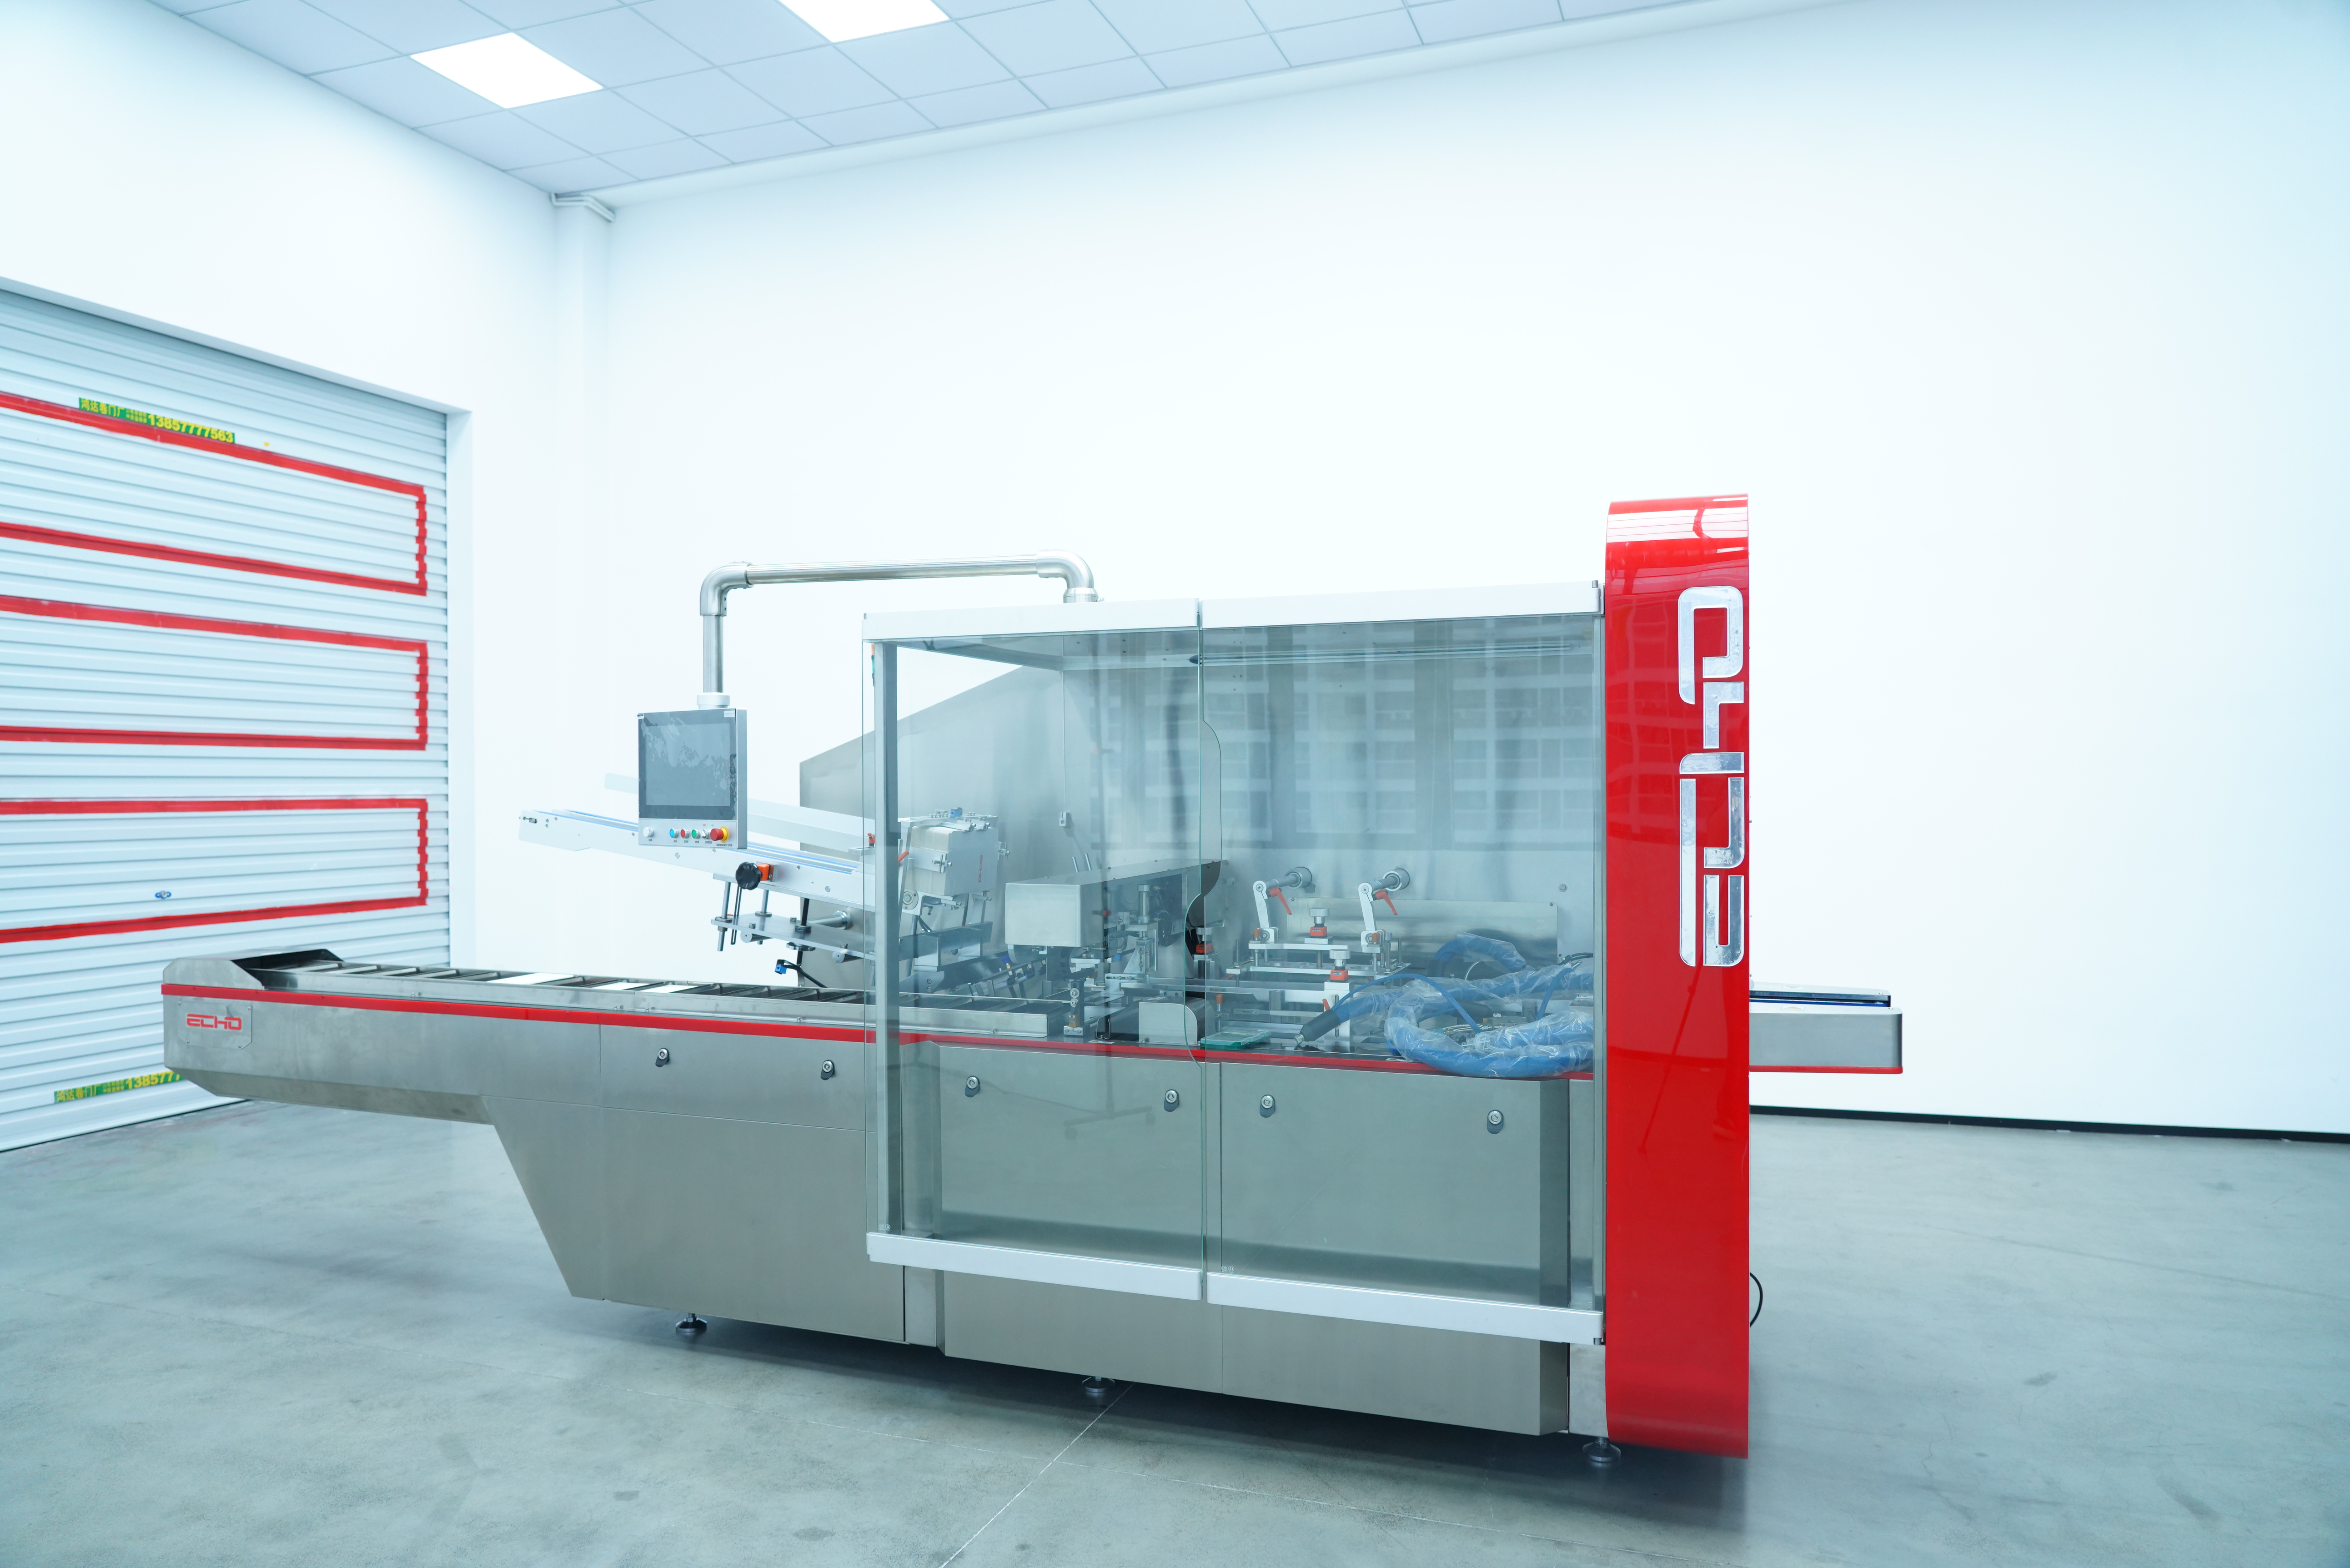
Selecting the right carton box packing machine can significantly impact production speed, labor costs, and packaging consistency. The market offers diverse options ranging from semi-automatic systems for smaller operations to fully integrated carton box packing machine solutions for high-volume facilities. This comprehensive guide explores the main categories of carton box packing machine technology, helping you understand their capabilities, applications, and suitability for different manufacturing environments.
Semi-automatic carton box packing machine systems require operator involvement but significantly reduce manual labor compared to entirely hand-packed operations. These carton box packing machine units typically feature operator-controlled feeding mechanisms where workers place items into the machine, which then automatically seals, closes, and ejects the packed cartons. This carton box packing machine category works well for businesses with moderate production volumes, seasonal fluctuations, or product lines requiring frequent changeovers.
For companies transitioning from manual packing, a semi-automatic carton box packing machine presents an affordable entry into mechanized packaging. The carton box packing machine investment remains reasonable while delivering measurable productivity gains and improved package consistency. Many facilities choose this carton box packing machine type as a stepping stone before committing to fully automated solutions, allowing them to evaluate workflow improvements and return on investment with lower initial capital expenditure.
Fully automatic carton box packing machine systems represent the pinnacle of packaging automation, requiring minimal human intervention after initial setup. These advanced carton box packing machine units continuously perform product feeding, box positioning, filling, sealing, coding, and output stacking without operator assistance. A comprehensive carton box packing machine of this caliber excels in high-volume production environments where consistent quality, speed, and efficiency directly impact profitability and market competitiveness.
Modern fully automatic carton box packing machine technology incorporates sophisticated sensors, programmable controls, and vision systems that adapt to different product dimensions and packaging specifications. The carton box packing machine systems can integrate seamlessly with existing production lines, upstream filling equipment, and downstream labeling or case packing operations. Many industrial-grade carton box packing machine solutions offer touchscreen interfaces, real-time diagnostics, and data logging capabilities that enhance operational visibility and enable predictive maintenance scheduling.
Vertical form-fill-seal carton box packing machine technology creates boxes directly from flat roll stock, fills them with product, and seals them in a continuous process. This carton box packing machine configuration proves especially valuable for products like powders, granules, liquids, and pre-portioned items where primary packaging flexibility matters. The vertical carton box packing machine reduces waste from pre-printed carton inventory while enabling rapid product or size changeovers through adjustable forming parameters and fill settings.
Horizontal carton box packing machine systems excel at handling fragile, oddly-shaped, or bulky items where gentle product handling and protective positioning are critical. This carton box packing machine type uses a horizontal loading axis that minimizes product tumbling and damage during the packing process. Beverage manufacturers, pharmaceutical producers, and specialty goods companies frequently rely on horizontal carton box packing machine equipment to maintain product integrity while meeting high throughput demands.
Industry-specific carton box packing machine designs address unique requirements across pharmaceuticals, food and beverage, consumer goods, and e-commerce sectors. Some carton box packing machine models feature pharmaceutical-grade validation, cleanroom compatibility, and documentation systems required for regulated environments. Specialized carton box packing machine solutions may include temperature control, inert gas injection, anti-static components, or tamper-evident sealing capabilities tailored to specific product protection and compliance needs.
Most manufacturers find that production volumes exceeding 5,000 to 10,000 units monthly make a fully automatic carton box packing machine financially viable, though this threshold varies based on product complexity, labor costs, and available capital. Even modest production volumes can justify carton box packing machine investment if labor availability is limited or packaging consistency requirements are strict. Smaller operations often achieve positive returns through reduced labor costs and improved quality consistency despite lower throughput compared to large-scale facilities.
If your operation requires frequent product line or package size changes, semi-automatic or flexible carton box packing machine systems may offer faster, simpler changeovers than rigid fully automatic equipment. Advanced carton box packing machine models now feature quick-change tooling and programmable configurations that minimize downtime between different products. Evaluating your actual changeover frequency and duration helps determine whether investing in rapid-adjustment carton box packing machine capabilities justifies the additional cost.
Fully automatic carton box packing machine systems typically require more sophisticated maintenance protocols and potentially higher technical support costs compared to simpler semi-automatic units. However, modern carton box packing machine technology increasingly includes predictive maintenance features and condition monitoring that reduce unexpected downtime. Selecting a carton box packing machine from manufacturers offering strong local support, comprehensive training, and readily available spare parts ensures long-term operational reliability and total cost of ownership advantage.

2026/09/20
Premade Pouch Machines: Reduce Film Waste, Cut TCO & Achieve Faster ROI

2026/09/20
Cut Premade Pouch Machine Changeover Time by 40% with Proven Best Practices

2026/09/20
Premade Pouch Machines: Boost Throughput, Cut Waste & Improve ROI

2026/09/20
Rotary vs Inline Premade Pouch Machines: Speed, ROI & Scalability Compared

2026/09/20
Premade Pouch Machine: Boost Throughput, Cut Labor Costs & Improve Seal Integrity

2026/09/21
Premade Pouch Machine: Pouch Types, Materials & Filling Guide

